Thermal Paste Selection for Smartphone Thermal Management
Thermal Paste in a Smartphone: Managing a 12 W Burst Inside a 7 mm Chassis
A flagship handset dissipates three to five watts while a game runs, but it reaches ten to twelve watts for the first seconds of a burst, and the die is only 45 to 60 mm2. At 8 W sustained over 45 mm2 the flux is already close to 18 W/cm2, and during a burst it passes 25 W/cm2. The junction-to-ambient budget is roughly 45 to 50 K, of which the plastic-to-air path through a 7 mm stack claims most. Nothing here scales like a notebook: the surface the user's finger touches sits one millimetre behind the die, so every kelvin held at a thermal paste joint is a kelvin visible on the outside of the product. Smartphone thermal management is therefore not a steady-state calculation with a burst margin; it is a burst calculation with a comfort limit.
Two joints carry the burst, and they are not the same joint
Most phone stacks contain far more interfaces than the two that deserve a thermal interface material. The die is bonded to a shielding frame or directly to a vapour chamber; the chamber or an aluminium bracket is then bonded to the mid-frame. Between those two hops and the glass cover there are gaps, adhesives and air that no paste can rescue, and specifying a thermal interface material there wastes thickness.
| Interface | Sustained flux | Burst flux | Bond line |
|---|---|---|---|
| Die to shield frame or vapour chamber | 8–15 W/cm2 | 20–30 W/cm2 | 20–30 µm |
| Vapour chamber or bracket to mid-frame | 4–8 W/cm2 | 10–15 W/cm2 | 30–50 µm |
| Mid-frame to display backlight side | 1–3 W/cm2 | 3–5 W/cm2 | Adhesive, not paste |
| Back glass to air and hand | Below 1 W/cm2 | Below 2 W/cm2 | None |
The first row is where a thermal interface material earns its place, and the second row is where it protects the vapour chamber from being fed heat through a bad contact. Below that, heat is a spreading and surface problem, and adding paste to a 1 W/cm2 joint only adds mass and volatile inventory — the reason smartphone thermal management is mostly a chassis discipline.
Why 20 to 30 µm, and why a thermal paste joint cannot be replaced by a pad
A phone gives the interface about 0.1 mm of budget between the die and the shield, and the stack above it is a display, a battery and a glass back, none of which tolerate preload. A 0.5 mm pad is not a compromise for a thermal paste joint; it is a different product. At burst flux the difference is not academic.
| Option | Bond line | Rise at 25 W/cm2 | Verdict for a phone |
|---|---|---|---|
| Thermal paste, 0.03 °C·cm2/W | 20–30 µm | 0.75 K | Correct on the die |
| Thermal paste, 0.080 °C·cm2/W | 30–50 µm | 2.0 K | Correct on chamber to frame |
| Gap filler, 0.5 mm at 5 W/m·K | 500 µm | 12.5 K | Consumes the entire burst margin |
| Graphite or graphene film | 30–70 µm | Spreads, poor bonding | Above the frame, not on the die |
Five field constraints a datasheet will not tell you
Pressure comes from adhesive, not screws. A modern phone is closed with glue and a few clips, so die pressure is set by the bracket's spring rate and often lands between 5 and 10 psi, unevenly across a 45 mm2 die. A joint qualified at 30 psi describes a different product.
Board warpage after reflow. A 0.6 mm main board can bow 30 to 60 µm through soldering, and the paste joint must absorb that bow without becoming a wedge that is thick on one side and starved on the other. This is a placement and stiffener question as much as a material question.
Burst-driven pump-out. This is the specific failure mode of smartphone thermal management: each burst expands the stack by tens of microns and pushes the bond line outward; hundreds of cycles per day for three years move paste away from the centre. A paste with high thixotropy and low oil separation survives this better than a low-viscosity one with a better catalogue number.
Optics and antenna keep-out. In smartphone thermal management the top of the board is crowded: camera modules with OIS, a periscope and antenna windows share it. Siloxane from a silicone-based thermal paste deposits on lens coatings and on antenna carriers, so volatility has to be specified, not assumed.
Drop and torsion. A 1.5 m drop transfers shear through the stack, and the paste joint is the softest layer in it. A cured adhesive joint can crack; a non-curing paste redistributes. The paste also has to survive the cleaning solvent used before display lamination.
Choosing the grade by joint, not by headline conductivity
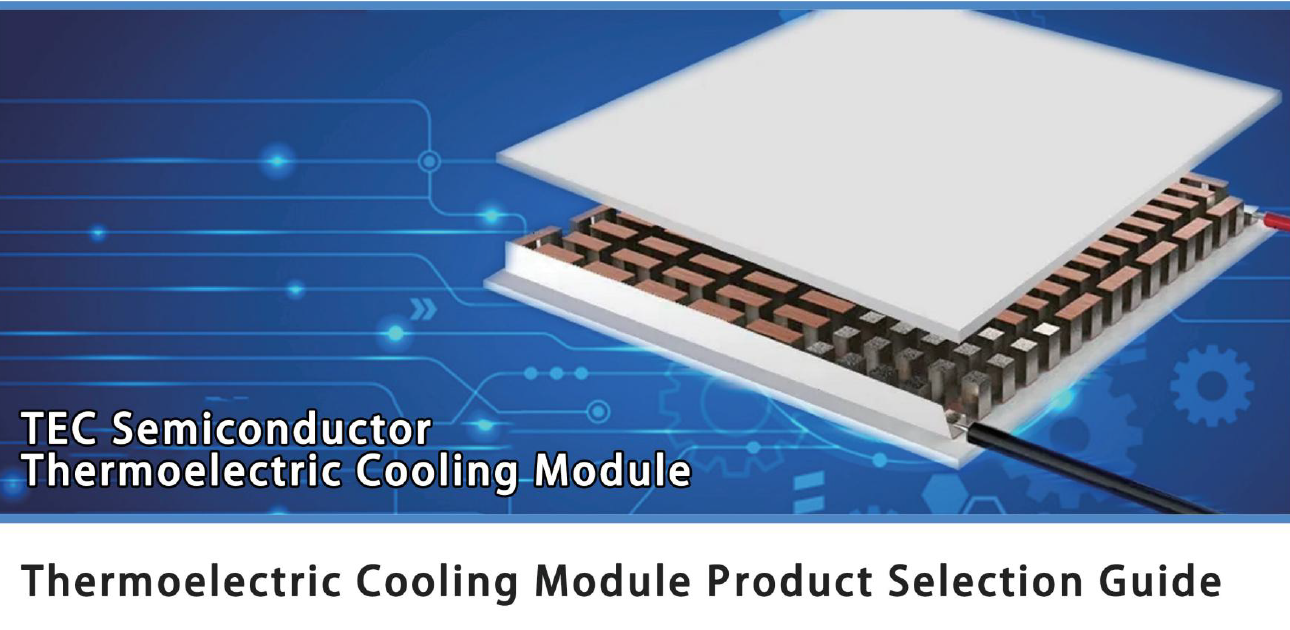
The TSAD Series from TOUSEN is a solvent-free, non-curing, thixotropic gray paste covering 1.2–6.5 W/m·K, with measured impedance of 0.201 to 0.03 °C·cm2/W at 30 psi, specific gravity 2.5–2.9 g/cm3, and a 12-month shelf life. In a phone the useful question is which grade of thermal interface material holds the thinnest stable joint at the pressure the bracket actually delivers.
| Grade | W/m·K | Impedance @ 30 psi (°C·cm2/W) | Density (g/cm3) | Typical phone position |
|---|---|---|---|---|
| TSAD60 | 1.2 | 0.201 | 2.5 | Shield to bracket, low-flux fill |
| TSAD66 | 3.5 | 0.080 | 2.7 | Vapour chamber to mid-frame |
| TSAD66-P | 4.0 | 0.070 | 2.6 | Rougher bracket or warped board area |
| TSAD83 PLUS | 5.2 | 0.050 | 2.6 | Main SoC at 3–5 W sustained |
| TSAD88 PLUS | 5.2 | 0.030 | 2.9 | Printed joint on a bare die in a thin stack |
| TSAD90 | 6.5 | 0.030 | 2.7 | Gaming handset, 8 W sustained |
| TSAD100 | 6.5 | 0.030 | 2.8 | Highest burst flux with the tightest target |
The dispense is a mass, not a dot
At 2.8 g/cm3 a 25 µm joint needs about 7 mg per cm2. A 45 mm2 die therefore takes 3 mg, and a 60 mm2 one about 4 mg. In smartphone thermal management that margin is the whole difference between a 25 µm and a 60 µm joint, and a 0.1 mg balance costs less than one reworked main board.
Print where the footprint is defined
For shield frames and vapour chamber contacts with a fixed outline, stencil printing the thermal paste at 0.1 mm with 80–90 percent coverage gives a repeatable 25 µm joint and removes operator variance from a line that produces thousands per day. Dispensing stays on the bare die, where the deposit must follow a small outline and the volume is only a few milligrams.
Where a pad still belongs
Between the battery and the frame, around antenna carriers and behind the camera module, a thin pad or a gap filler does the job: those joints exist to absorb tolerance and to spread, and they never see 20 W/cm2. Putting paste there adds a migration path and no thermal benefit.
Qualification that mirrors how a phone is used
The only meaningful test of smartphone thermal management is a burst sequence: 500 cycles of ten seconds at 12 W followed by twenty seconds at 2 W, recording both junction and back-cover temperature, because the second value triggers throttling in the user's hand. Repeat impedance on a sacrificed unit after the cycling. Then add 500 hours at 60 °C and 90 % RH, a 1.5 m drop sequence on six faces, a 150 °C gravimetric oil separation test, and an outgassing check if a camera or antenna shares the volume. The 12-month shelf life matters on a phone line because paste is often staged beside the SMT line.
Assembly and service rules
- Clean the die and shield with isopropyl alcohol; a residue under a 25 µm joint is a local hot spot that shows up as a dropped frame, not as a failed test.
- Keep the print inside the die outline by 0.2 mm; thermal paste beyond the outline adds no conduction and feeds migration into the shield cavity.
- Apply the bracket with a controlled force and check flatness, not torque; the joint reads the pressure distribution, not the number on the tool.
- On rework, remove the old film fully and reprint; two layers of paste read worse than one fresh layer at this thickness.
- Store cartridges closed, below 30 °C, away from flame; the product is non-hazardous but its rheology drifts if left open.
Conclusion
Smartphone thermal management is decided in the first ten seconds of a burst, when the flux reaches 25 W/cm2 and the junction budget is only about 50 K. The thermal paste joint cannot rescue a chassis that spreads heat badly, but it is the one element the assembly process still controls after the industrial design is frozen, and at 25 W/cm2 the difference between 0.03 and 0.080 °C·cm2/W is more than a kelvin. Specify the joint by its flux, size the deposit in milligrams, print where the outline is defined, and qualify at the pressure the glue line actually produces rather than the 30 psi of the datasheet.
Impedance data, grade table and packaging options for the paste described above are published on the TSAD Series thermal paste product page, and samples for print trials on your own shield frame can be requested there.
Thermal Paste Selection for Tablet Thermal Management
Related Article